

Programming While Cutting: How Vigour Maximises Productivity with hyperMILL®
Vigour Limited | Coventry, United Kingdom
Key Takeaway
By building its manufacturing operations around hyperMILL® from day one, Vigour has created a safe, reliable and highly productive 5-axis machining environment. Parallel programming, collision-checked processes and advanced machining strategies keep the spindles turning while enabling the company to manufacture complex, tightly toleranced components that other suppliers often avoid.
Founded in 2015, Vigour Limited has grown from a single 5-axis machining centre into a specialist trusted with some of industry’s most demanding components. From the outset, the business has relied on OPEN MIND Technologies' hyperMILL® CAM software to produce the complex, tightly toleranced parts that define its reputation.
After a career spanning subcontract machining and Formula One, Ashley Hatton, Founder and Managing Director of Vigour had already spotted the gap he wanted to fill. “Lots of subcontract manufacturers had 3-axis machining, and they were mostly programming at the control. Adoption of 5-axis and CAD/CAM was barely in existence in the subcontract market”. Where most new machine shops start with 3-axis capability and work up, Coventry-based Vigour went straight in at 5-axis. Today, the company operates four full 5-axis machines; three are DMG MORI EVO50 machines with automation - a deliberate choice that builds process consistency across the shop floor.
“My business is built around hyperMILL®; it's been a pillar of success for the company. It really is the backbone of the business.”
Ashley Hatton, Managing Director Vigour Ltd.
Building the Business on Reliability from Day One
When it came to choosing a CAM system, Ashley didn't need to run an exhaustive evaluation. “I looked at one or two other CAM vendors at the time, but hyperMILL® was the safe choice. I'd used it previously at Formula One teams, and it was very reliable. It’s incredibly safe; the cycles are fast to calculate – it's reliable and robust.”
That reliability has underpinned the growth of the entire ISO: 9001-accredited business. “My business is built around hyperMILL®; it's been a pillar of success for the company. It really is the backbone of the business, and we now have two seats with a full suite of additional features.”
Keeping the Spindle Turning While Programming the Next Operation
The clearest illustration of hyperMILL®'s impact on Vigour's throughput is how Ashley sequences his day. Rather than programming a part from start to finish with the machine sat idle, he breaks the job into roughing and then finishing stages. Roughing is programmed in around 15 minutes, and the machine is then set up with a billet and runs the part. Once up and running, the detailed features and finishing operations are programmed and sent to the machine – maximising spindle utilisation.
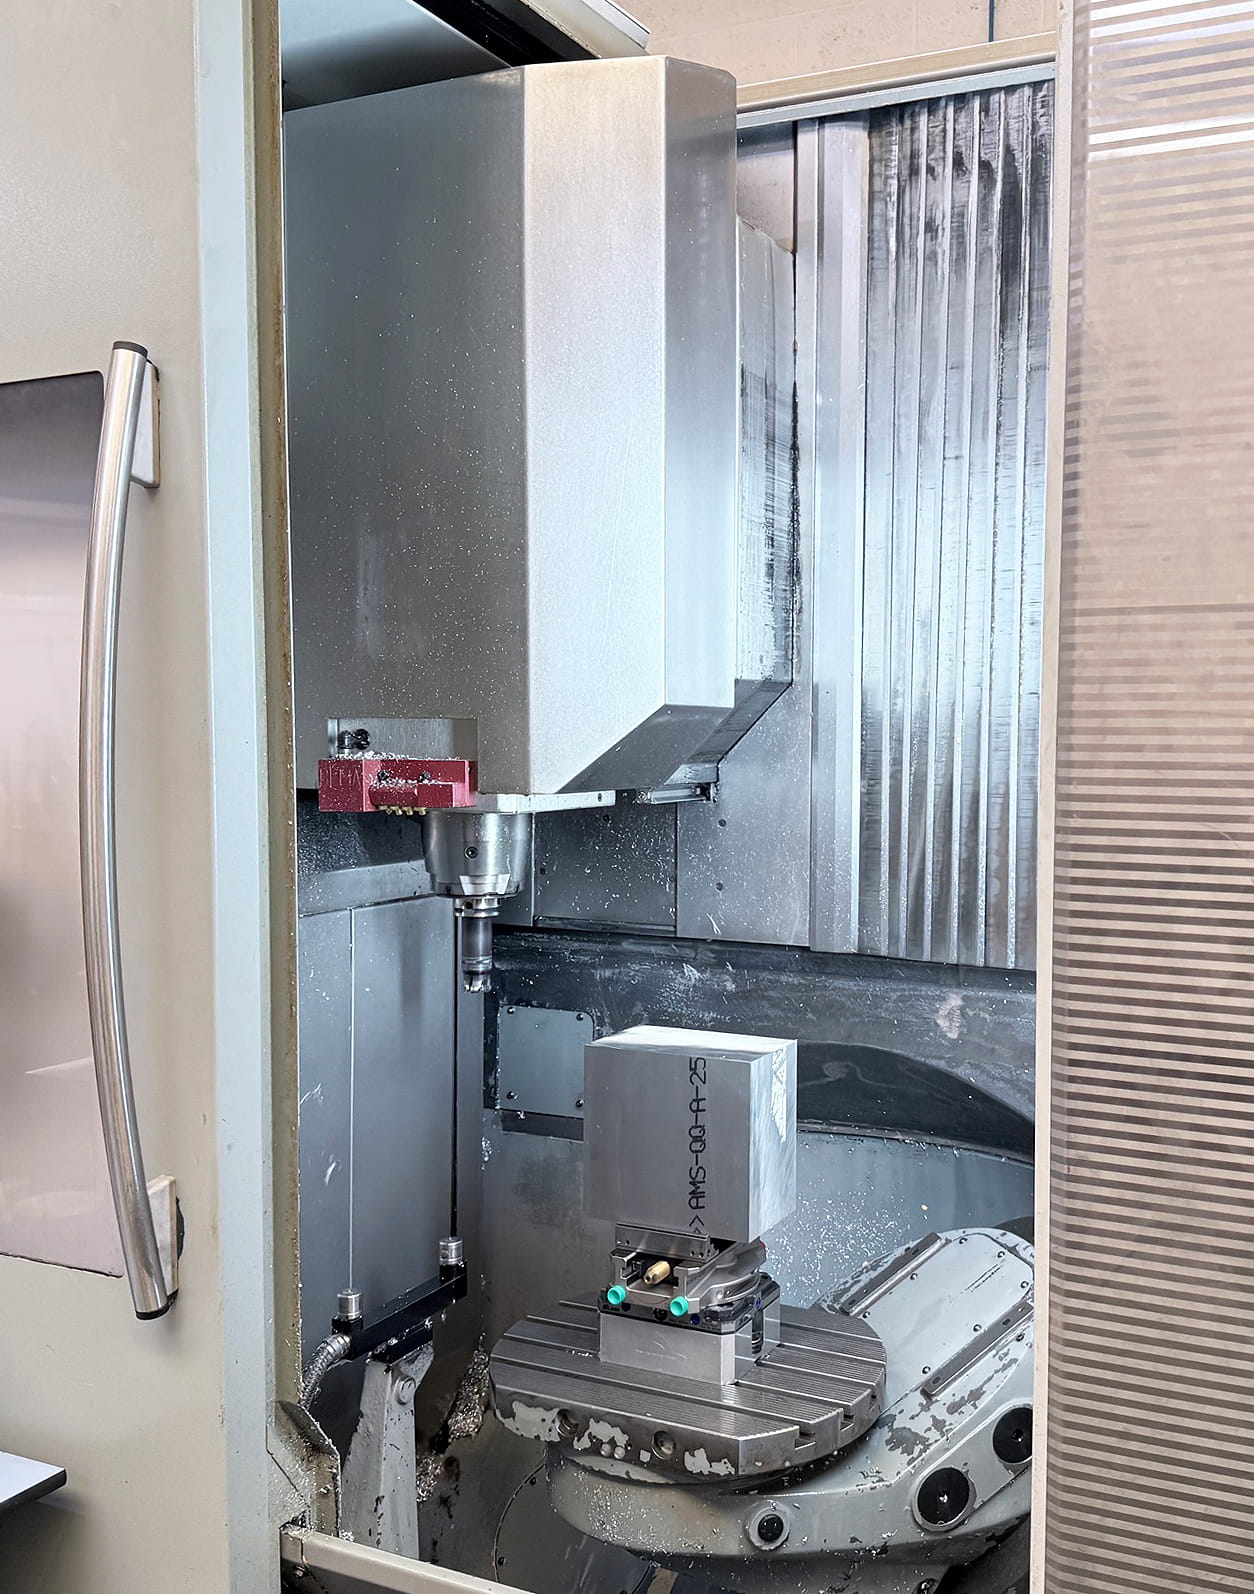
A billet ready for machining on a DMG MORI EVO 50 at Vigour
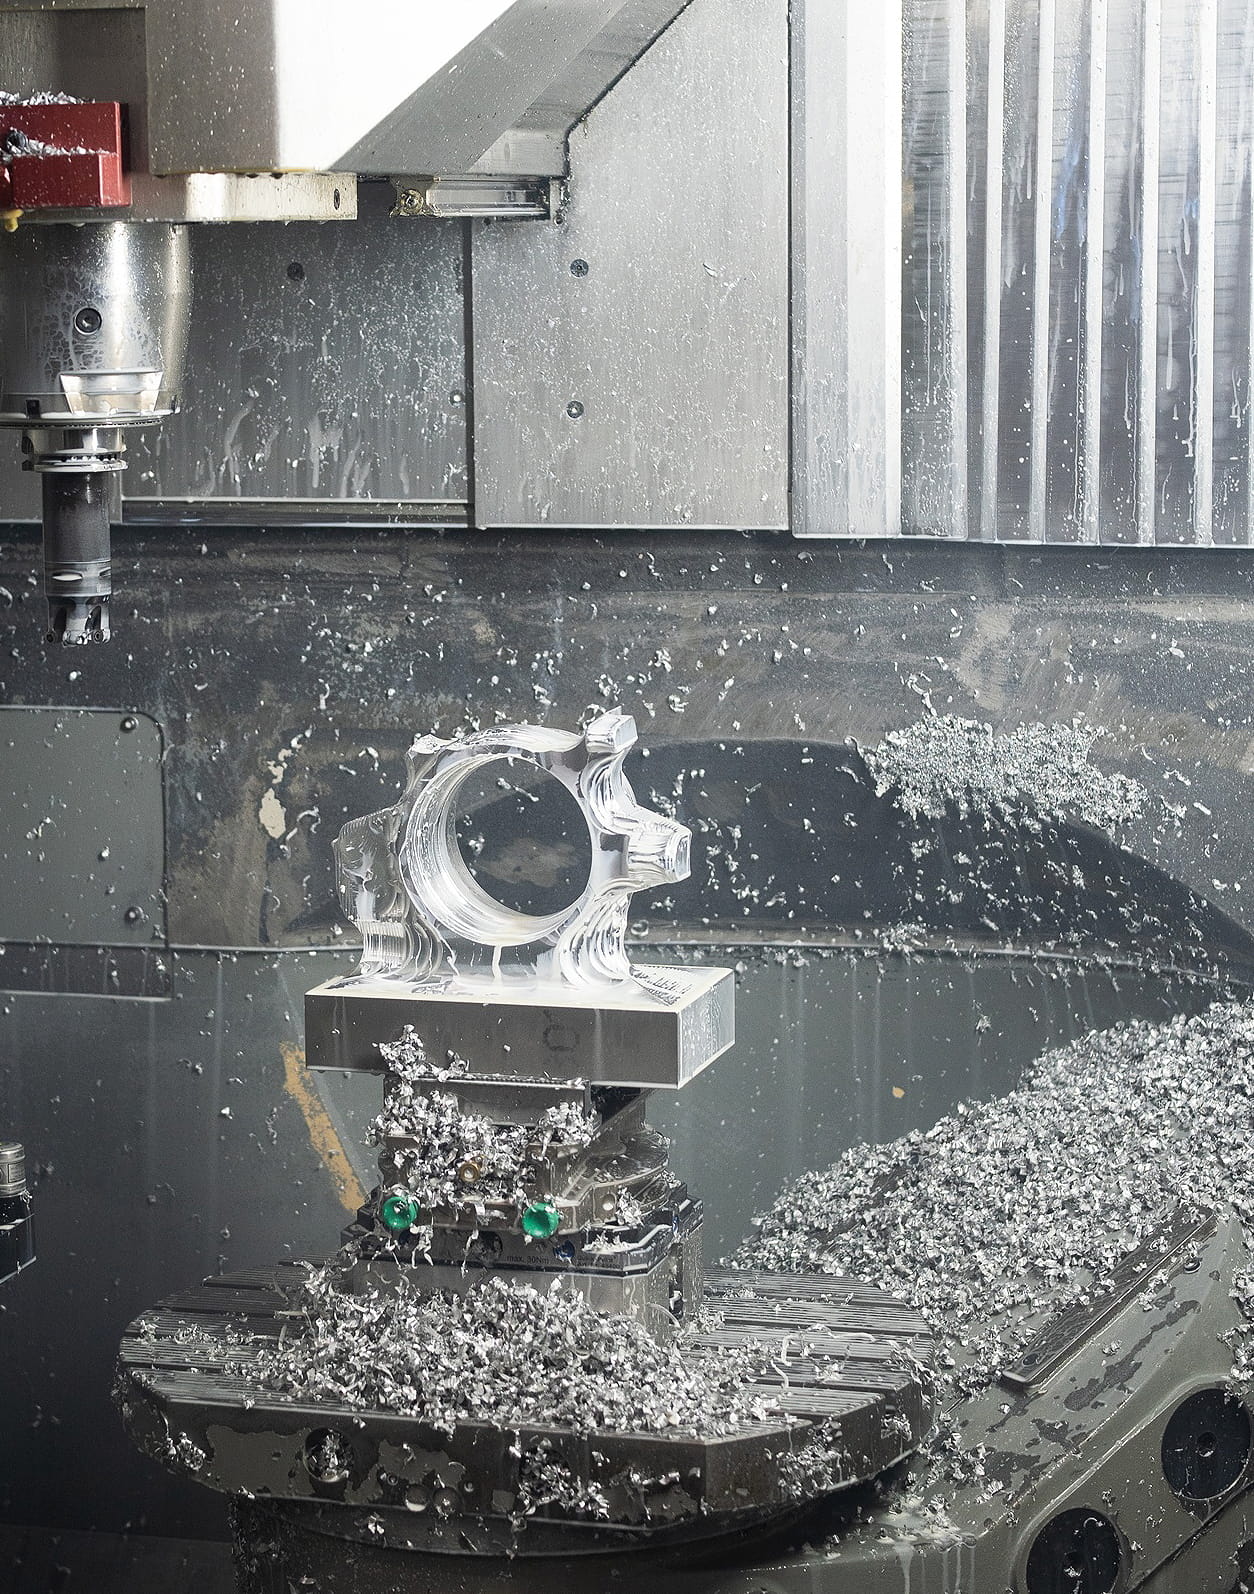
A motorsport part being machined on the DMG MORI at Vigour
It starts the moment an RFQ is won. A script automatically creates the correct file path on Vigour's network, and hyperMILL® points directly to the STEP file. Ashley adjusts the work plane to match the stock, then hyperMILL®'s boundary box function fits a box around the whole part with a single click – deriving stock size and vice position. He also adds extra surfaces to the model to represent workholding, “not something everyone does,” he notes, but a step that helps the simulation account for the vice itself, not just the part.
With the block loaded, Vigour typically works through a facing sequence before the main roughing begins. “I hit the button, go to Z -5mm, flip the frame, and set -5mm to skim 5mm of stock from each face of the billet, establishing clean, known reference surfaces before committing to the finished geometry. Parts are then probed, tools are laser-set, and we press go.”
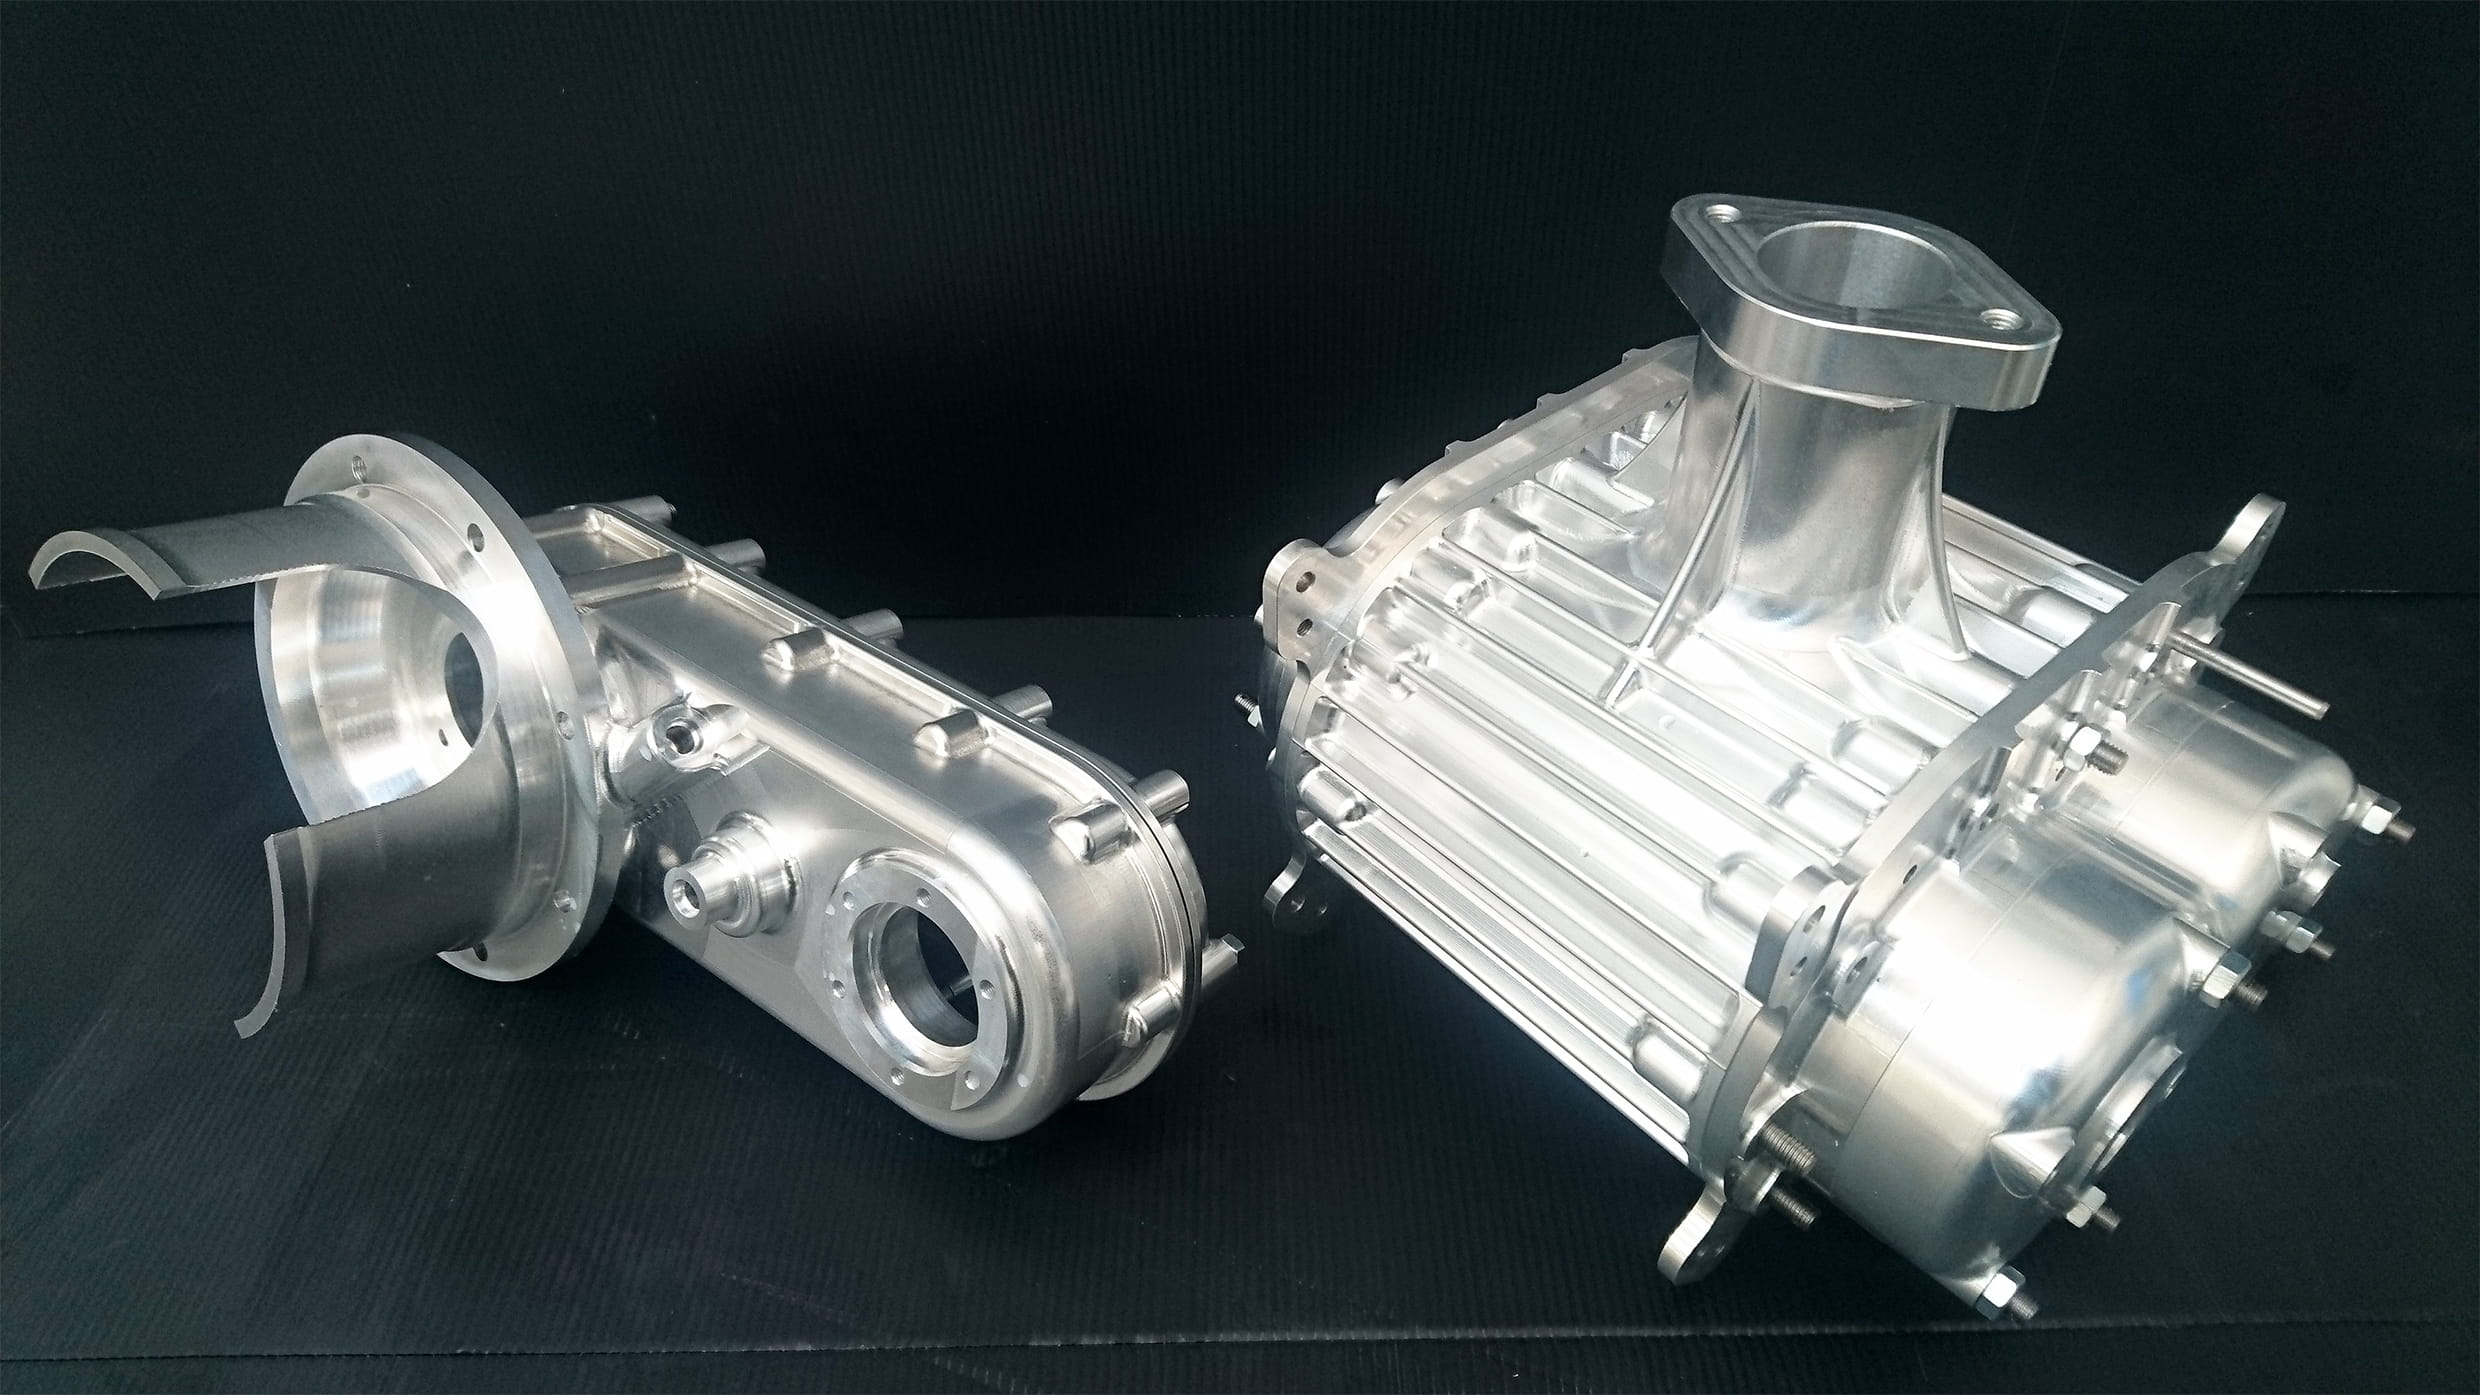
A motorsport supercharger and gear drive manufactured at Vigour with hyperMILL®
Preparing the Next Stage While Production Continues
The next stage of programming starts while that first pass is running. Ashley is already back at the screen, programming the second roughing operation – typically using the same Sandvik 42mm button cutter for high-feed milling, followed by a 12mm R1 ball nose end mill for a deep step-down, then a 6mm R2 for a shallow contouring pass, leaving around 0.25mm on the part, ready for finishing.
The roughing stage takes about 40 minutes to reduce the part to its smallest dimensions, often as tight as 3mm. While that's running, finishing operations are programmed using hyperMILL®’s Z-Level Finishing for the larger surfaces, the Profile Finishing function for the part walls, and ISO Machining to work methodically through the pockets – all while the machine is still cutting the previous stage. “The machine is always running in the background,” he says. Apply that logic across every stage of every part, and the cumulative saving across a busy shop floor is substantial.
None of this would be possible without confidence in the simulation. “There's no single-blocking or prove-outs anymore,” Ashley says. “We run the simulation in the software. Once it's gone through that with no collisions, it's on the machine and running, and I sit down and start programming the next lot of roughing or finishing. Then, the Feature Recognition tool for finishing enables us to select the part and feature map the holes. It all just takes two minutes. We couldn’t imagine life without hyperMILL®.”
Taking On the Parts Other Manufacturers Avoid
Vigour's reputation is built on parts that other shops shy away from. “I want to do the parts that other people don't want to do,” Ashley says. “I see the company as an engineering solution provider, not a manufacturing business. If you've got really challenging parts, difficult metals, difficult geometry – that's where we sit.”
The business has now developed a reputation within the gas turbine sector. Recent projects have included the manufacture of MAR-M247 cast turbine wheels and highly complex 17-4PH H900 compressor wheels for micro gas turbine applications. These rotating assemblies require exceptionally tight geometric control, with shaft-to-wheel runout figures less than 5 microns across the complete assembly, levels of precision typically associated with aerospace and defence hardware.
A car upright, manufactured for the Oxford Brookes Formula Student team, demonstrates the point. Tightly toleranced, with angled holes and undercut walls, the part demands a combination of 5-axis Shape Finishing, ISO Machining inside pockets, and Automatic 5-axis Rest Machining. “hyperMILL® makes sure the toolholder doesn't come into contact with the job, and the cutting edge is always in cut – so you don't get chatter, just sublime surface finishes.”
The company has also introduced its Vigour Roadmap to Employment and Alternative Route to University Programme, delivered in partnership with Solihull College. Apprentices undertake a structured four-year pathway while gaining meaningful industrial experience. The programme has been designed to allow young engineers to earn, learn and develop practical manufacturing expertise within a high-performance engineering environment.
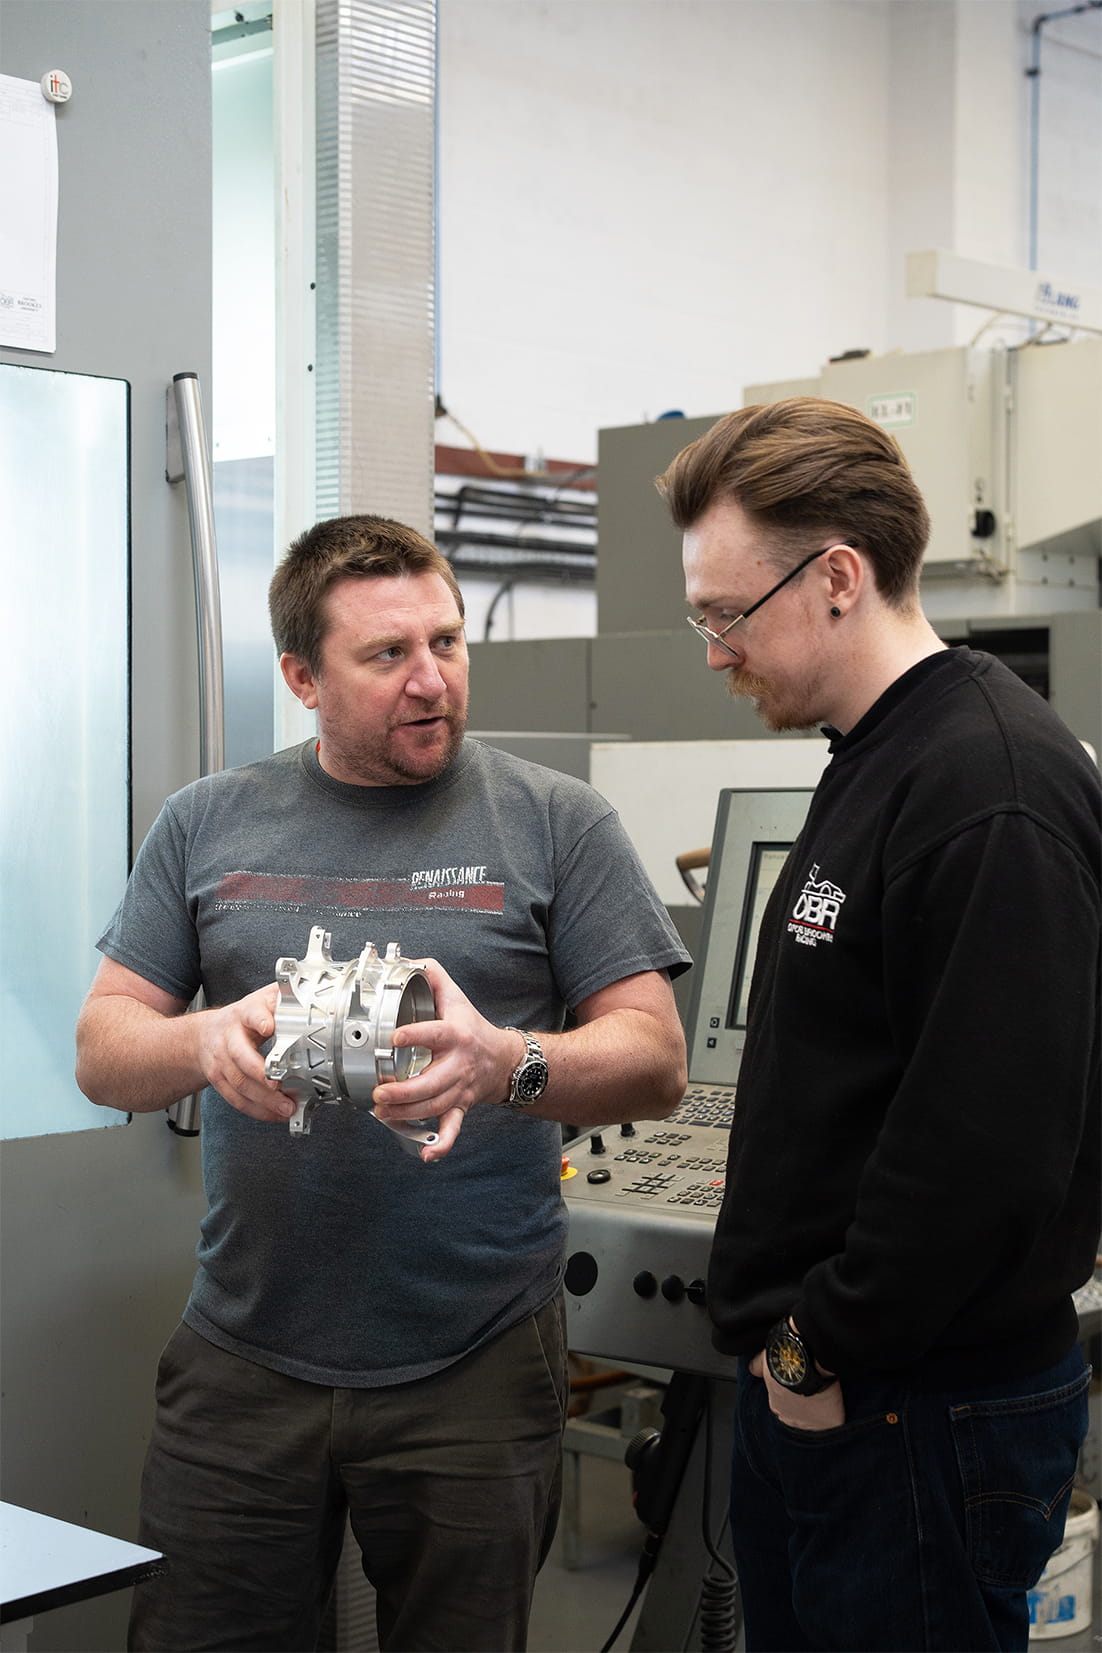
Ashley Hatton, left, with a student from Oxford Brooks Racing Team
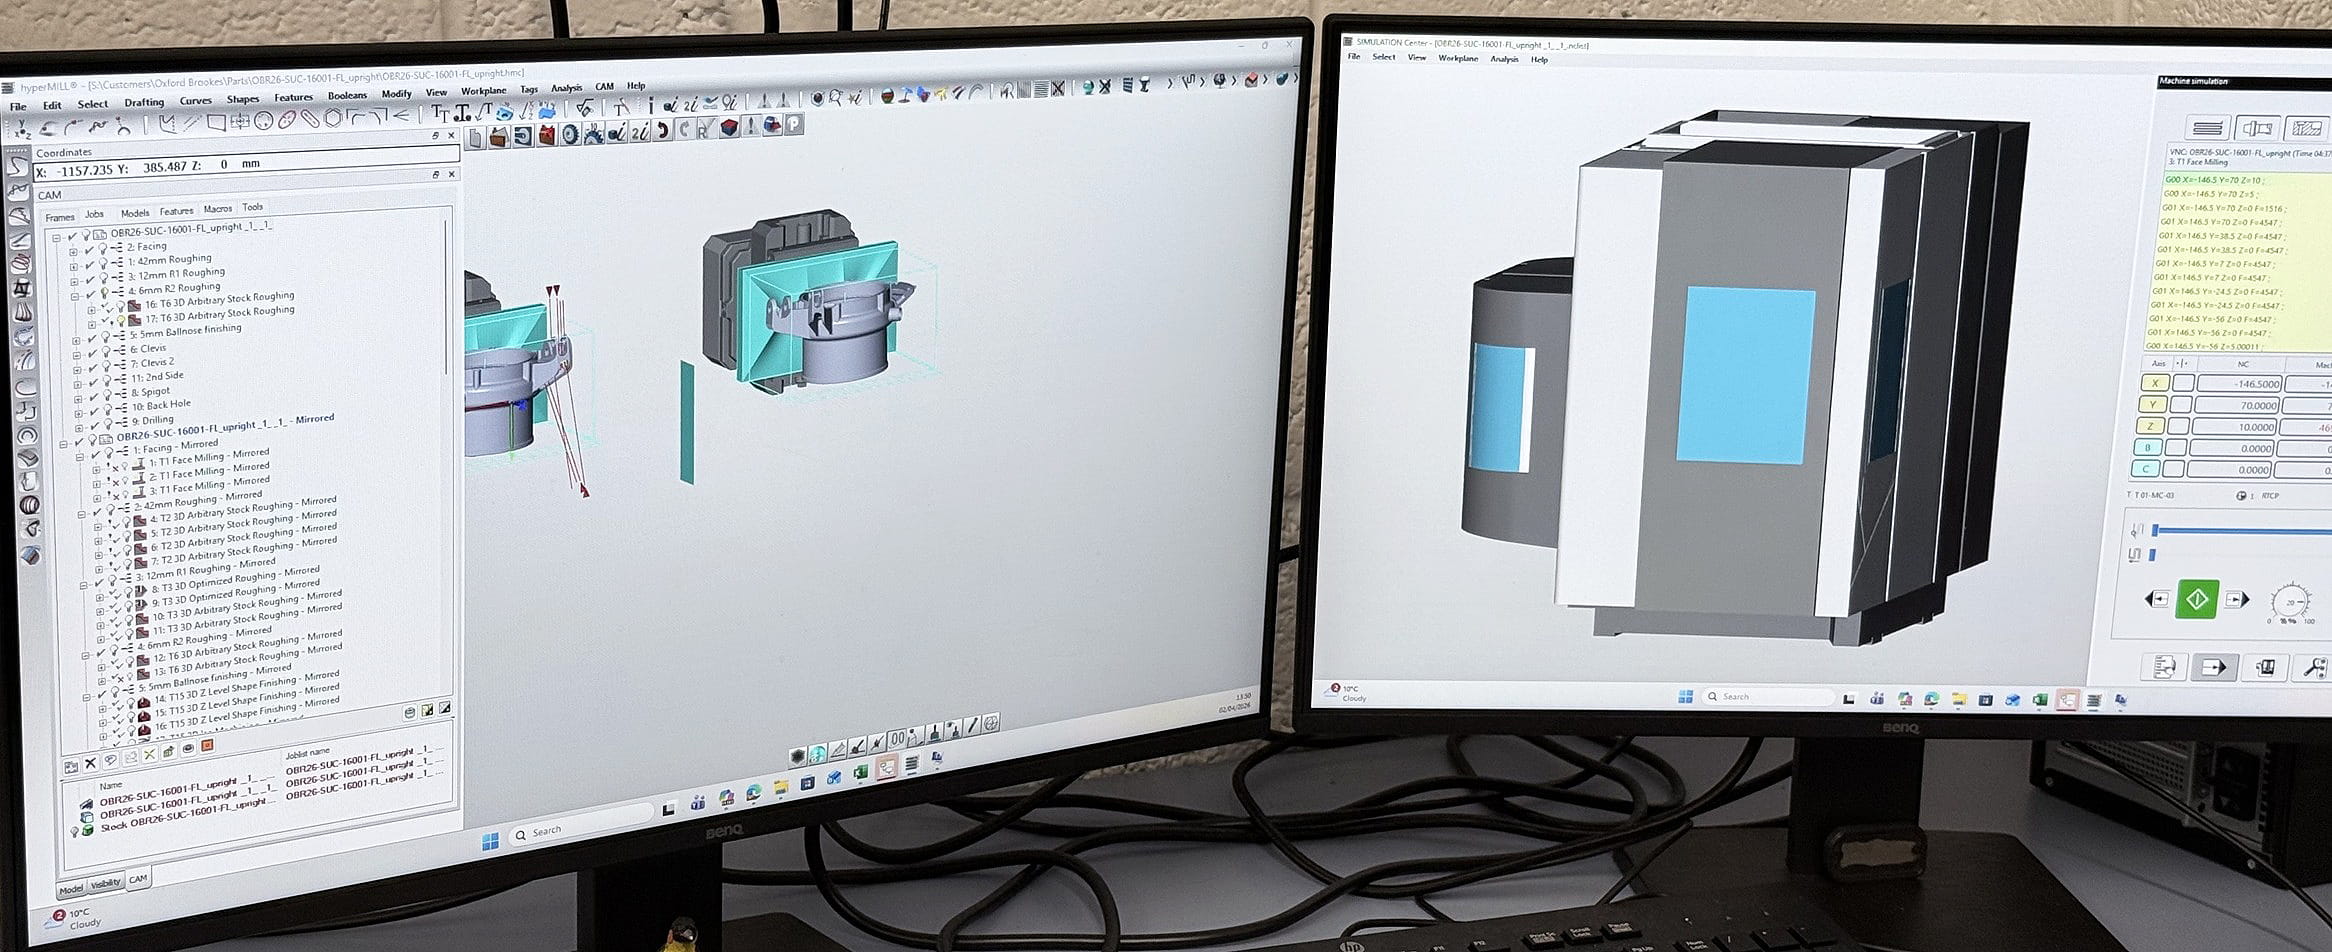
Vigour relies on hyperMILL®’s 5-axis technology to program a motorsport upright
From 8 Hours to 5: Faster Machining and Exceptional Surface Finish
Among the hyperMILL® strategies that have made the biggest impact at Vigour is Tangential Plane Machining with barrel tools. “We’ve used barrel tools for around eight years. We were making a motorsport upright, and the part was taking eight hours,” Ashley recalls. “We introduced barrel tools and hyperMILL® Tangential Plane Machining; it wiped out three hours of cycle time with exceptional surface finishes. We’ve been using it ever since.”
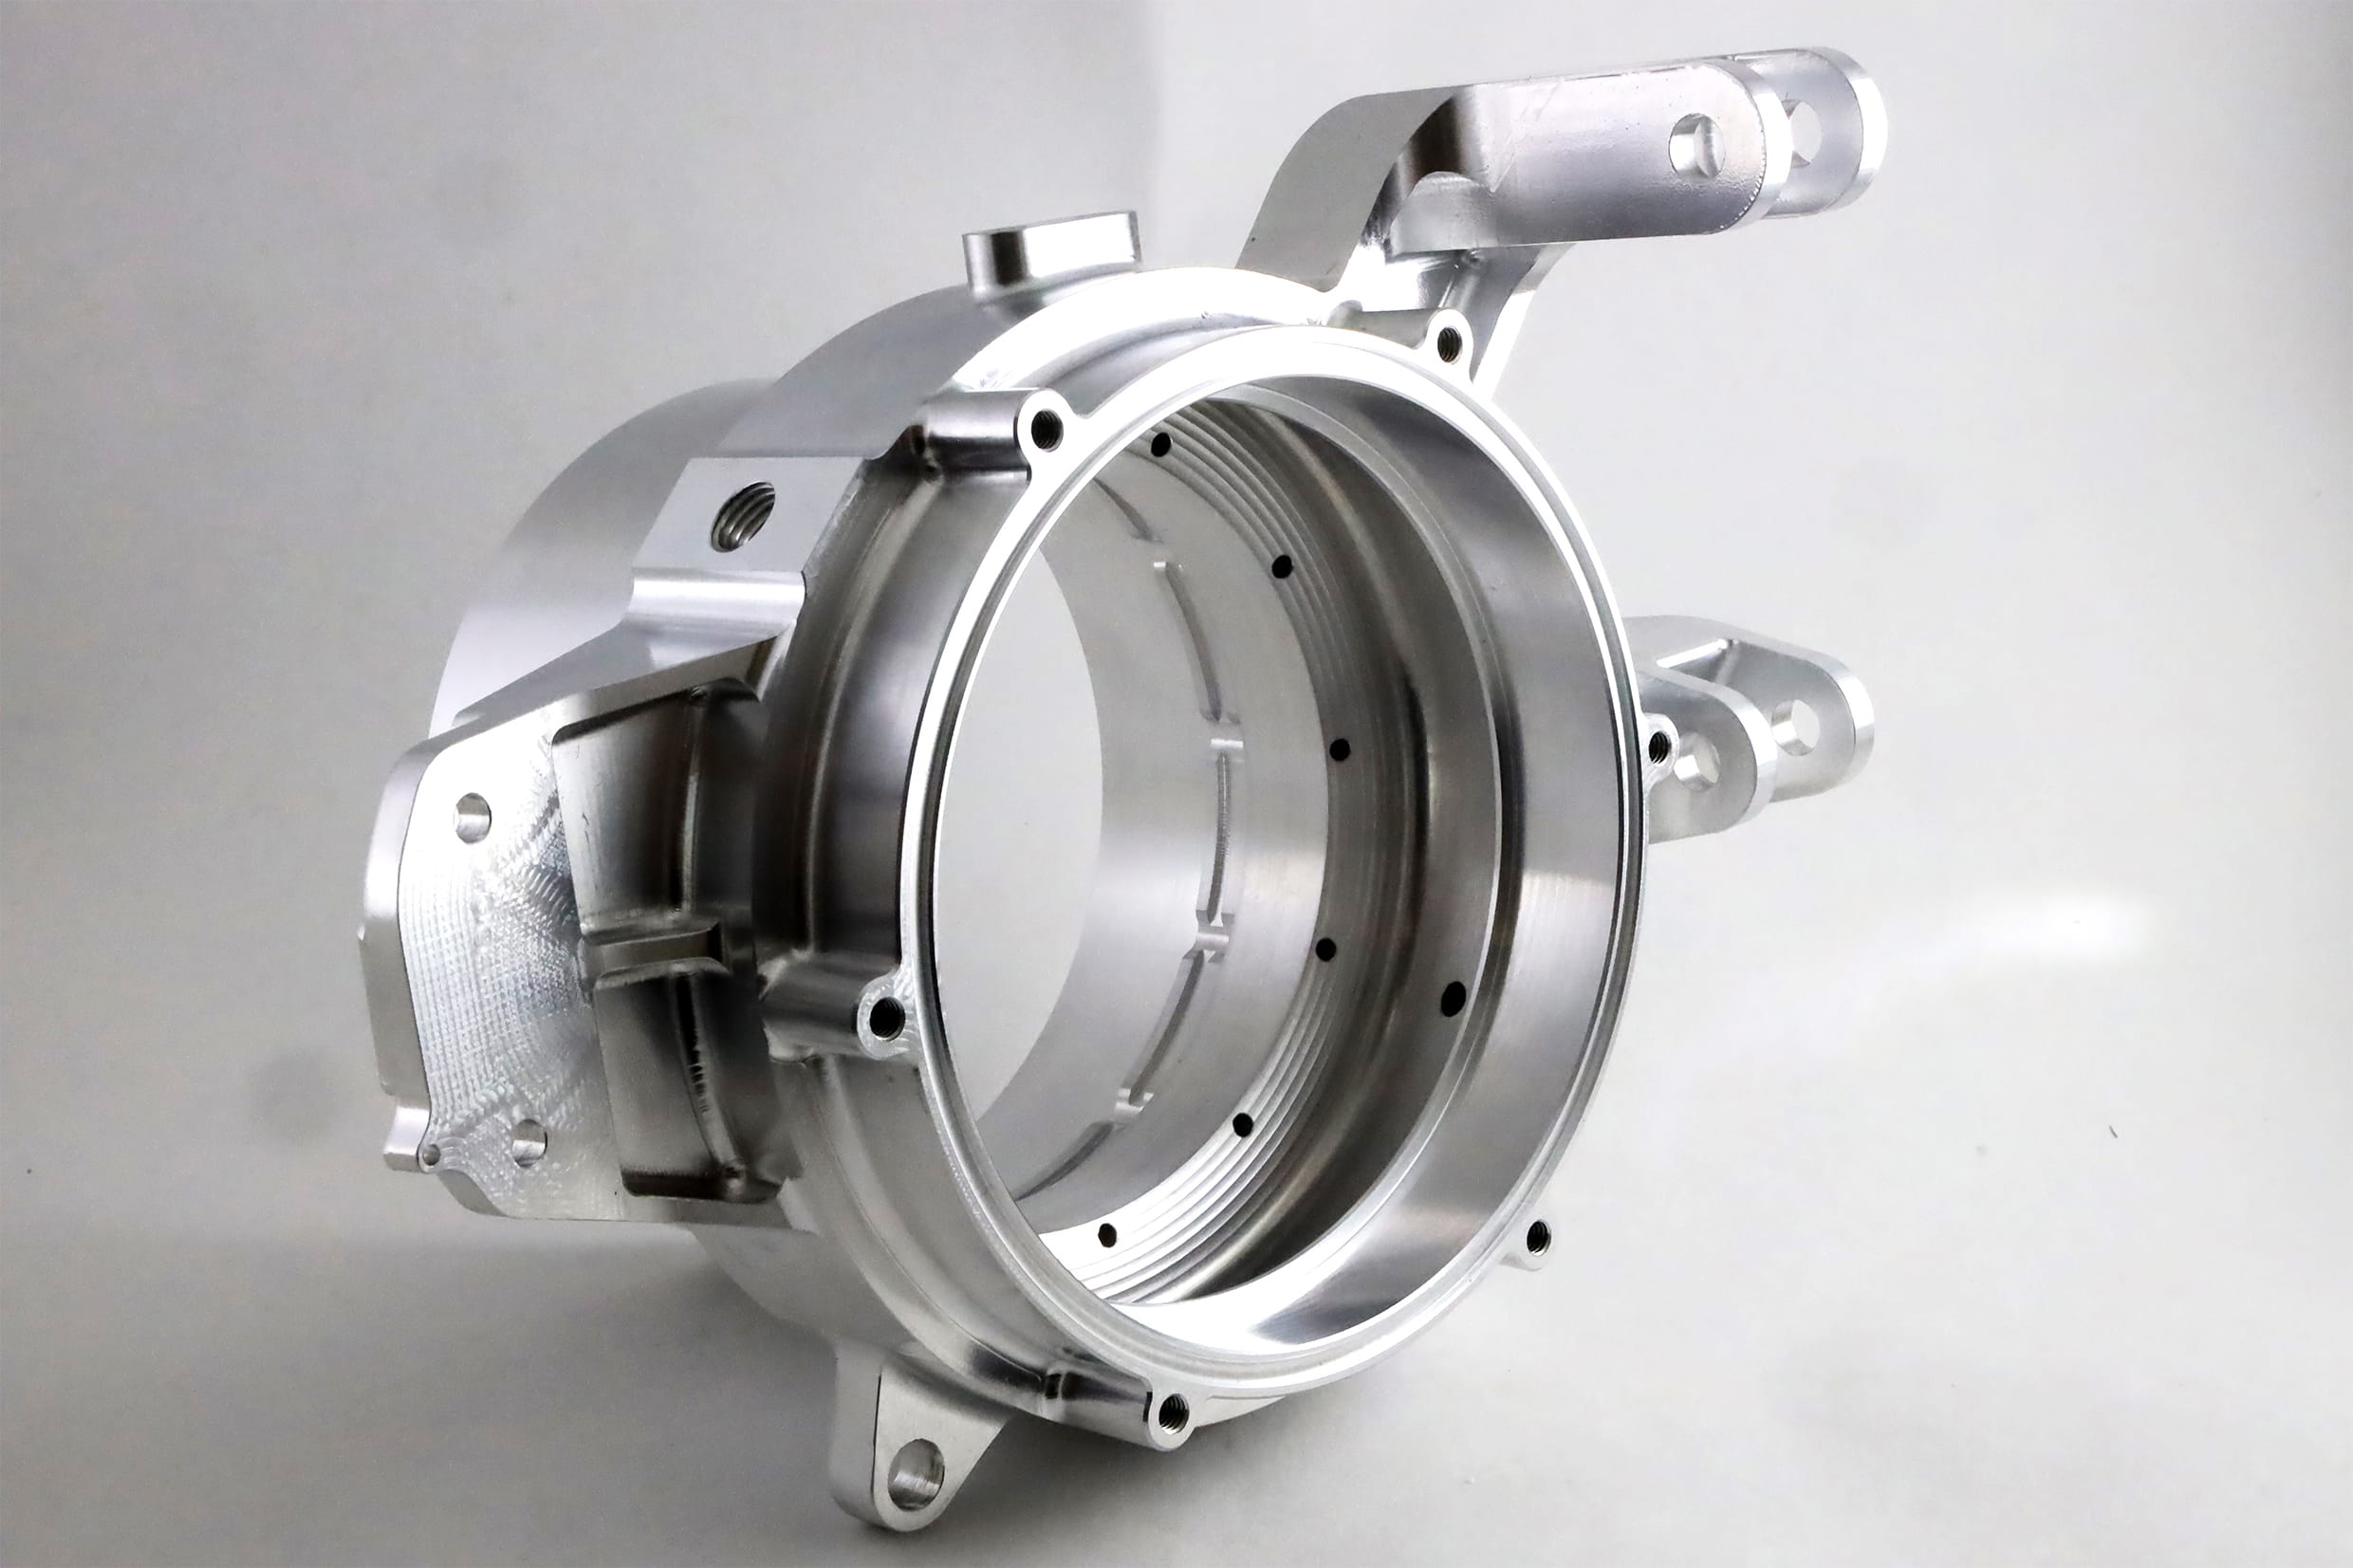
Motorsport upright part manufactured for a student racing team at Vigour
When Customer Feedback Becomes Product Innovation
Ashley's relationship with OPEN MIND stretches back to 2010, when he first requested custom fields in the hyperMILL® tool database while working at a Formula One team. “Everyone who's run a machine shop knows about the tool library and the Excel spreadsheets, and the mess that ensues,” he says. OPEN MIND's Ken Baldwin took the request to the development team, and the functionality was added. Vigour is now using that same custom data to build its own in-house ERP system, tracking stock quantity, location and price. “That's a real example of where they've taken on board what you've said and actually added functionality to the software, which I'm using today and really appreciate.”
Service support is just as responsive in day-to-day business. “Within the hour I'll get an answer to a question. If I call up, quite often I'll get a response immediately.” For a business whose growth has been so closely tied to its CAM platform, that support and forward trajectory matters. “It's very difficult to say where Vigour would be today without hyperMILL®,” Ashley concludes, “but where it is today is a success due in large part to hyperMILL®.”